High Speed Hollow Wall Winding Pipe Machine: Boosting Efficiency in Pipe Production
2026-11-16
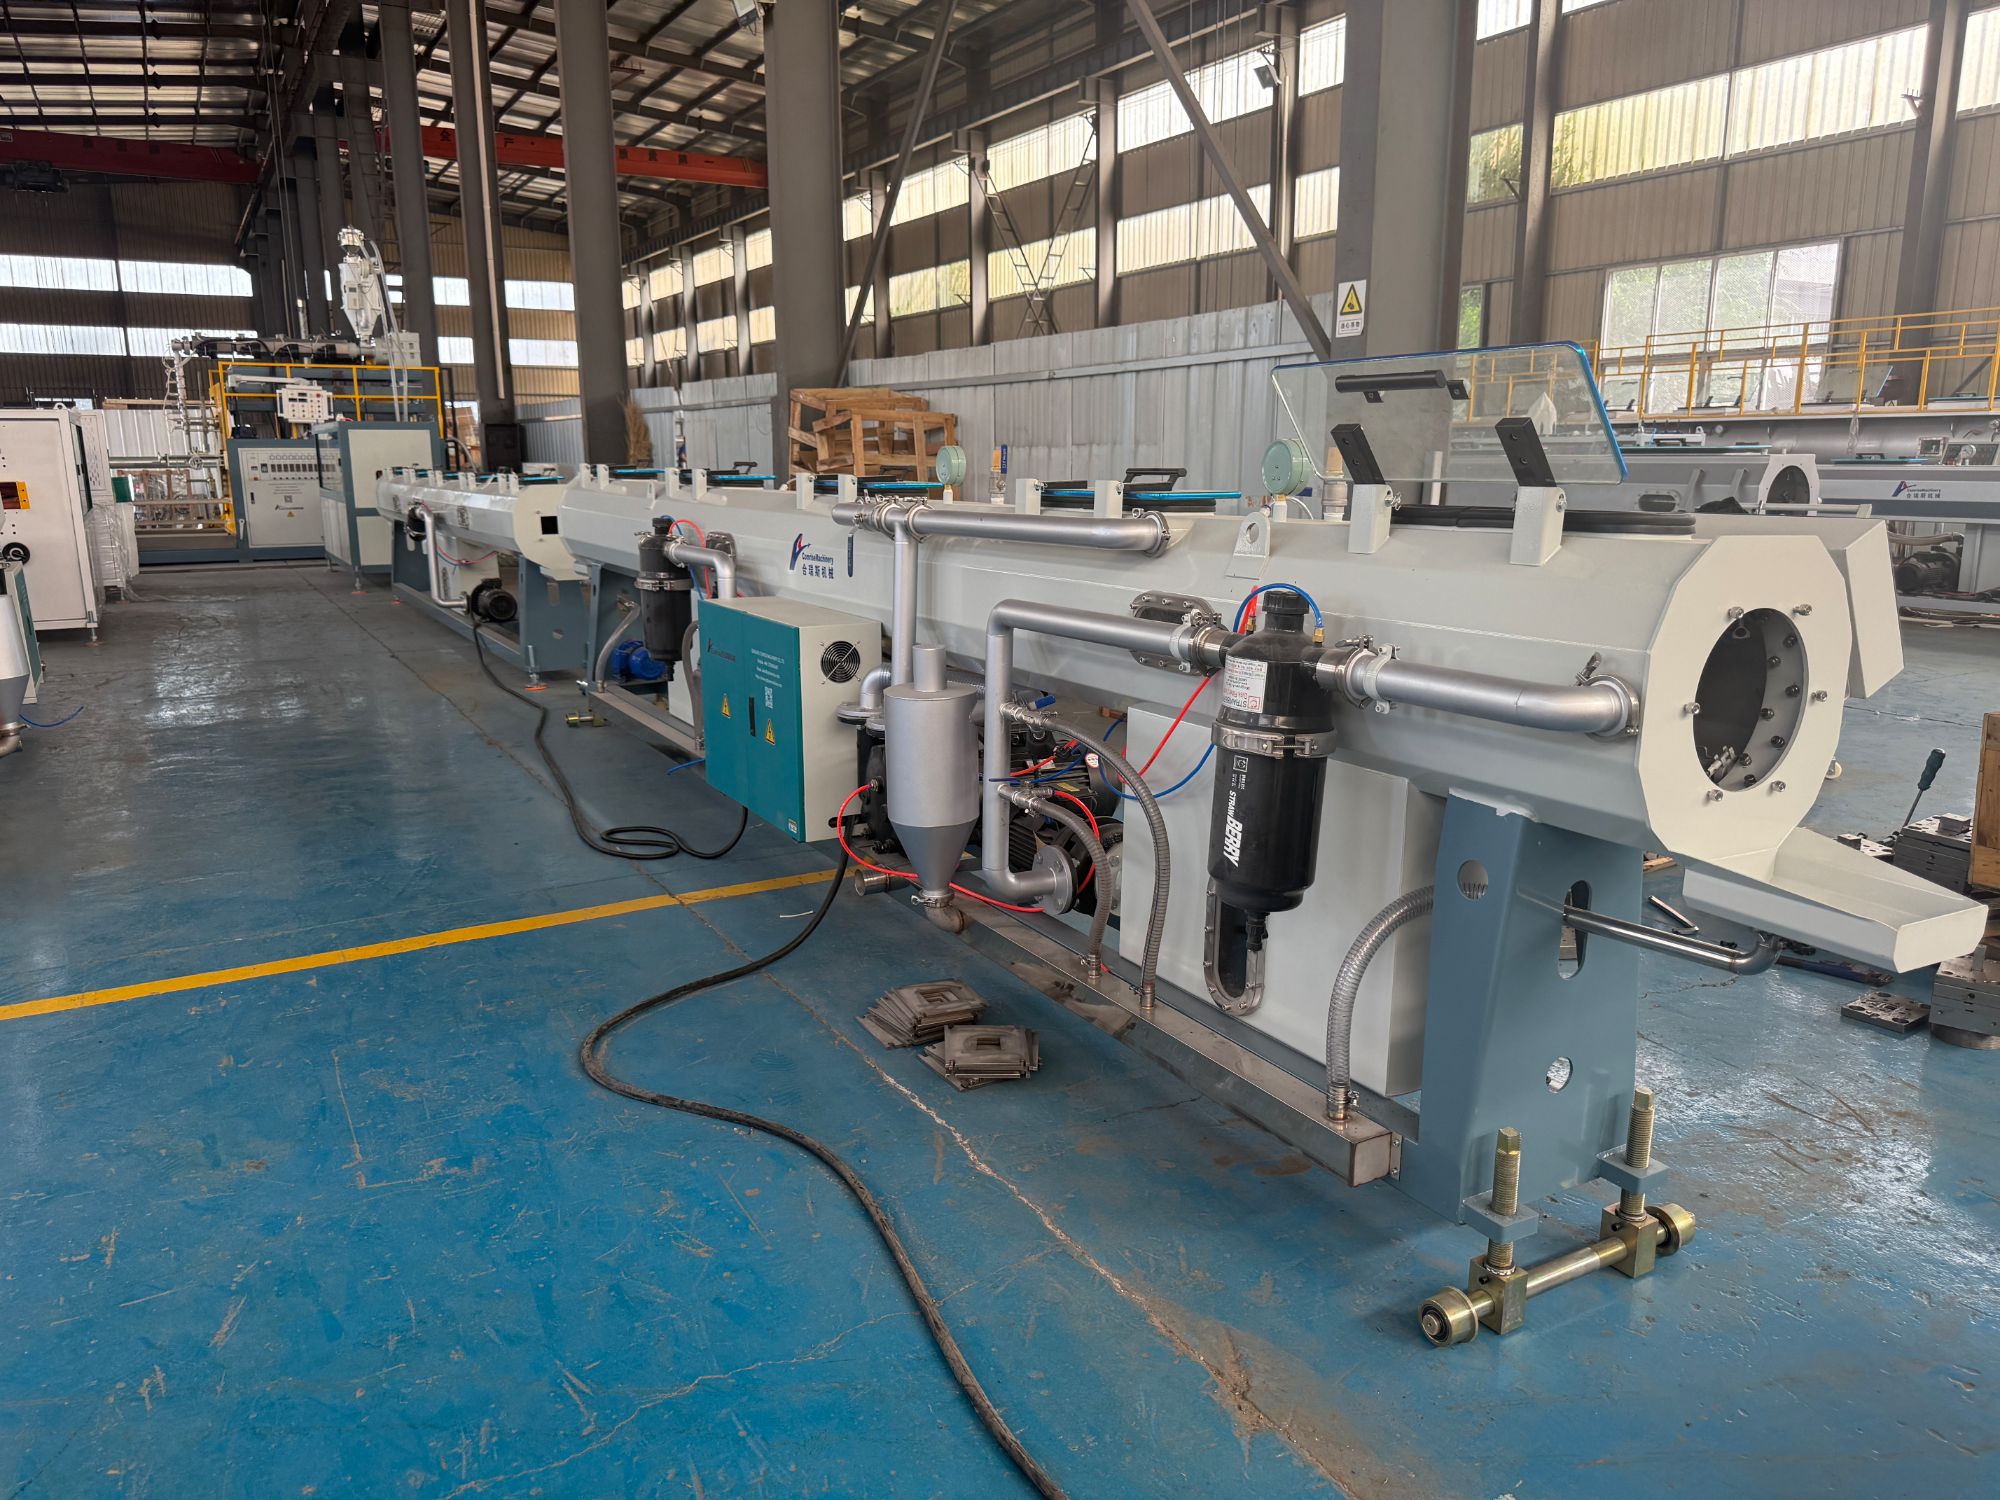
Pipe production often gets bogged down by slow winding speeds and frequent stoppages—problems that quietly eat away at profitability. The high-speed hollow wall winding pipe machine tackles this head-on, delivering faster cycles and more consistent wall thickness than conventional methods. What makes it stand out? The engineering behind COMRISE, a name synonymous with reliable pipe machinery. In this post, we’ll break down how this machine boosts efficiency and why it’s becoming a go-to choice for forward-thinking manufacturers.
Where Higher Spindle Speeds Meet Consistent Hollow Wall Formation
Running a spindle at higher rpm usually invites chatter, thermal expansion, and uneven material removal—all of which quietly erode wall consistency in hollow components. Here, the spindle's acceleration profile is tuned to match the natural frequency of the tool-body system, so the cutting edge stays in a predictable orbit even as speed rises above the standard threshold. Bore roundness and wall thickness repeatability don't fall off a cliff when the dial moves past 8,000 rpm.
What separates this approach is the direct link between spindle load feedback and feed override. As the cutter moves through interrupted cuts or varying cross-sections, the control adjusts axial feed in microsecond increments. This prevents momentary dwelling that can shave a thin spot into the inner wall. Paired with a variable-helix tool that distributes radial load more evenly, the hollow cross-section holds its intended thickness without relying on slow semifinish passes.
In practice, that means fewer rejected blanks after boring or drilling operations. The wall maintains a consistent gauge around the full circumference, and surface finish remains clean enough to skip a secondary honing step in many cases. Higher spindle speeds no longer force a trade-off between cycle time and dimensional integrity—both move in the same direction.
Cutting Cycle Times Without Compromising Layer Bond Strength
Reducing cycle times in additive manufacturing often feels like walking a tightrope between speed and structural integrity. The conventional approach of simply cranking up print speeds tends to leave layer adhesion trailing behind, creating weak points that compromise the final part. What gets overlooked is that the real bottleneck usually isn't the extrusion rate itself, but how heat is managed between passes. By focusing on the thermal history of each layer, you can push speeds higher while giving the polymer chains enough time to entangle across the interface. It's less about fighting the machine's limits and more about finding the sweet spot where cooling and deposition meet.
One practical route involves tuning chamber temperature and cooling fan behavior to keep the previous layer near its glass transition temperature just before the new bead lands. This prolongs the window where molecular diffusion can occur, even if the printhead is moving faster. Another angle is adjusting line width and layer height ratios, so that the contact area between layers grows without requiring a slower travel speed. These aren't exotic tricks; they're small, deliberate changes that shift the trade-off curve in your favor. The result is a process that holds up under mechanical testing, not one that merely looks fast on a spec sheet.
The key is to treat cycle time reduction as a system-level problem rather than a single parameter tweak. Calibrating extrusion temperature to match the accelerated pace, for instance, can prevent under-extrusion at corners while maintaining strong fusion at the interface. Build plate adhesion also plays a supporting role, keeping the first layers anchored so that higher speeds don't induce warping or delamination. When these elements work together, you get parts that come off the printer sooner without sacrificing the interlayer strength that everyone worries about.
How Automated Tension Control Reduces Wall Thickness Variation
In any continuous extrusion or winding process, small shifts in material tension directly translate into dimensional drift. Automated tension control removes the guesswork by continuously monitoring pull force at the die or take-up stage and adjusting brake or drive torque in milliseconds. This closed-loop response keeps the material from thinning out under excessive draw or bunching up when tension drops, so the wall thickness stays within a much tighter band than manual adjustments ever achieve.
The real advantage comes from consistency across the entire run. Operators may set a baseline tension at startup, but heat buildup, spool diameter changes, and slight variations in feedstock all alter the effective load. An automated system compensates for these variables without waiting for a thickness gauge to flag a problem. By the time a manual correction would be made, several meters of off-spec product may already be produced. With automation, the correction happens before the variation becomes measurable.
In practice, this means fewer rejected coils, less material waste, and downstream processes that no longer need to accommodate unpredictable wall thickness. The data logging built into many automated tension controllers also helps engineers trace any residual variation back to a specific cause, whether it is a worn roller or an inconsistent feed rate, making the entire line easier to fine-tune.
Material Waste Drops When Winding Paths Adjust in Real Time
The moment a cutting head veers off its planned route, scrap starts piling up. But when the path recalibrates mid-motion—twisting around a knot in the wood or a hard spot in the steel—the offcuts shrink to almost nothing. It’s the difference between forcing a straight line through imperfect material and letting the tool breathe with the grain, shaving away only what’s necessary.
On a busy production floor, this isn’t a theoretical nicety. Sensors track the blade’s position a hundred times a second, comparing the live curve against the digital twin. A slight drift on the third bend? The software nudges the next pass a fraction of a millimeter inward, sparing the sheet from becoming another bin of wasted strips. Workers notice the quiet shift: fewer trips to the dumpster, more usable panels stacked at the end of the day.
The savings compound in odd places. Offcuts that used to be swept away now fit into smaller jobs—a bracket here, a shim there. Inventory stops ballooning with buffer stock meant to cover for rejected parts. And the machines, no longer fighting the material’s natural resistance, run cooler and longer. Real-time path adjustment doesn’t just cut down waste; it changes how a shop thinks about every raw sheet that rolls through the door.
Quick Diameter Changeovers for Short-Run and Mixed-Spec Orders
Switching wire diameter on a machine usually means stopping production, swapping guides, adjusting straighteners, and recalibrating pull rolls. For short-run work or orders where specs change from one coil to the next, that downtime eats into already thin margins. A dedicated quick-change concept starts with a tool-free clamping system for the prestraightener and roll cassettes. Instead of loosening bolts and re-aligning every pass, operators snap in a pre-set roll assembly sized for the next diameter. The key is keeping each cassette pre-loaded and tagged with the diameter and material type, so changeover becomes a matter of pulling one unit and sliding in another within two or three minutes.
The payoff shows up clearly on mixed-spec days. A shop running five or six different wire sizes across a single shift can lose an hour or more to traditional setup. With quick-change cassettes and diameter-specific guide inserts, the machine returns to production almost immediately. One practical approach is to color-code the tooling by diameter range and keep a small cart next to the line with the next job's cassettes, guides, and pressure rolls already staged. That way the operator never has to hunt for parts or make fine adjustments under pressure. Instead, they verify the tag, swap the assembly, and run a short test piece to confirm the finish and straightness.
For truly short runs—sometimes only a few hundred feet of a particular diameter—the economic case for quick changeovers becomes impossible to ignore. If a ten-minute setup eats into a fifteen-minute run, the job barely breaks even. But when the switch takes under three minutes, the same order becomes profitable. The same principle applies to mixed-spec orders where the wire diameter changes within a single production ticket. Machines equipped with modular draw blocks and snap-in straightener cassettes let operators move from one spec to the next without losing their place on the run sheet. It turns what used to be a scheduling headache into a continuous flow, and that flexibility is often what keeps small-batch work competitive against larger, less nimble suppliers.
Why Lower Vibration Levels Keep the Line Running Longer Between Stops
Vibration is often dismissed as background noise until a bracket cracks or a coupling works loose. Lower vibration levels remove that slow, cumulative damage from the equation. Bearings, mounts, and electrical connections stay within their designed load ranges, so the weak points that normally force a mid-shift shutdown simply don't reach failure as early.
There is also a control-side effect. Excessive vibration can trigger false signals in accelerometers or cause vision systems and laser alignment tools to drift out of tolerance. Once those readings become unreliable, operators pause the line for inspection or recalibration. With reduced vibration, the measurement drift is smaller, so the line holds its setup longer and stops become planned rather than reactive.
Less vibration also means fewer loose fasteners and less fretting on connectors. Maintenance teams aren't chasing random torque checks or replacing worn isolators every few hundred cycles. That shifts downtime from frequent short interruptions to longer, scheduled windows, which keeps throughput steadier across a shift.
FAQ
Instead of relying on a single solid-wall extrusion, it forms pipes by spirally winding a hollow profile and fusing the seams, which cuts material use and lets you run at higher line speeds.
The continuous spiral winding eliminates the need for heavy molds or slow cooling cycles, so manufacturers can switch diameters quickly and keep output consistent without long downtimes.
You'll see them in stormwater drainage, sewage systems, cable ducts, and agricultural irrigation, where large-diameter lightweight pipes are in demand.
Yes, most designs use adjustable winding cages or interchangeable mandrels, allowing quick size changes without rebuilding the whole production setup.
HDPE and PP are the usual choices because they weld well during winding and give the finished pipe good flexibility and chemical resistance.
The hollow ribs create a high section modulus, so the pipe stays stiff and resists crushing under soil loads while using far less polymer than solid-wall pipe.
Regular checks on the winding head alignment, roller bearings, and extrusion die lips are essential; keeping the melt temperature stable also prevents weld-line defects.
Compact models exist for smaller operations, but the real payoff comes with sustained runs of medium to large diameter pipe, so most buyers are mid-size to large producers.
Conclusion
The machine pairs higher spindle speeds with closed-loop tension regulation, so hollow wall thickness stays within tight tolerances even when line velocity climbs. The payoff shows up quickly in daily output figures. Operators can push cycle times down significantly because the winding head does not sacrifice layer bond strength for speed—the resin delivery and compaction rollers adapt dynamically to the faster lay-down rate. Automated tension control removes the guesswork from filament or tape payout, reducing wall thickness variation across the pipe circumference and along its length. The result is a structurally reliable product with fewer rejected sections and less rework. Operators no longer need to overbuild sections to hide inconsistency.
Real-time winding path adjustments trim material waste by altering the deposition pattern only where needed, rather than relying on fixed overbuild allowances. Quick diameter changeovers allow short-run and mixed-spec orders to flow through the same line without lengthy tooling swaps, which keeps utilization high for job shops and in-house producers alike. Lower vibration levels extend the interval between maintenance stops—bearings, guides, and mandrel supports all see less fatigue. Taken together, these improvements shift the bottleneck away from the winding station and toward downstream processes, delivering a faster, cleaner, and more predictable production environment.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com